





Four Important Precautions for Operating a Profile Bending Machine
Pre-Start Preparation
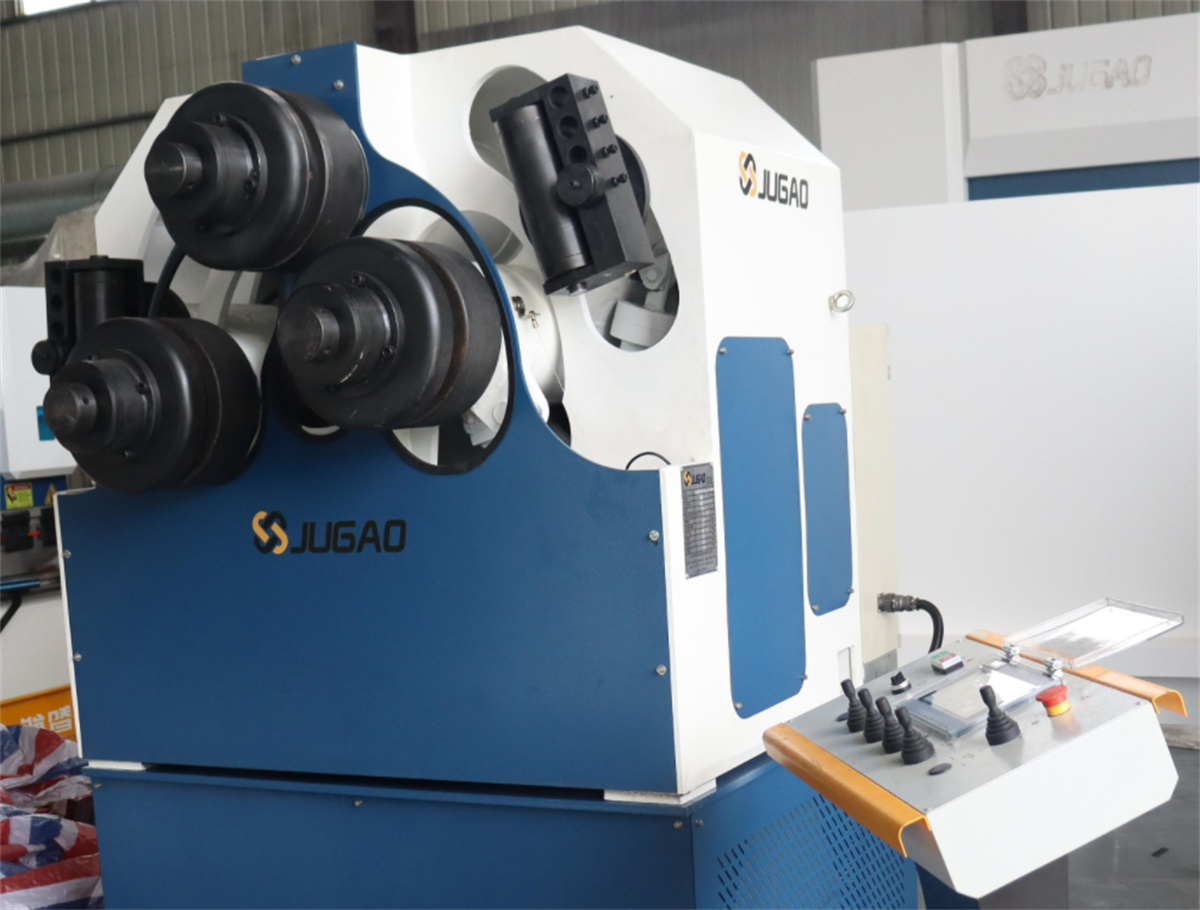
Equipment Inspection:
Check the hydraulic oil level, cleanliness, and for any leaks.
Check all fasteners (bolts, nuts) for tightness and looseness.
Check the electrical wiring for integrity, reliable grounding, and proper function of buttons, switches, and indicator lights.
Check all rollers (especially the upper and lower rollers) for correct positioning and obstruction.
No-Load Test Run:
After starting the equipment, run it under no-load for 1-2 minutes to observe smooth operation.
Let the upper slide plate complete 2-3 full-stroke reciprocating movements to ensure no jamming, abnormal noise, or unusual vibration.
If abnormal noise, odor, vibration, or hydraulic system leaks are detected, immediately stop the machine for inspection and troubleshooting. Operating a malfunctioning machine is strictly prohibited.
Precautions During Operation
Return to Origin Operation:
The return-to-origin procedure can only be executed when the upper slide plate and all positioning shafts are in their origin positions.
If the components are found to be out of position, they should be manually reset or brought back to their original positions via the control program before performing the return-to-origin operation to ensure processing accuracy and equipment safety.
Operation Control:
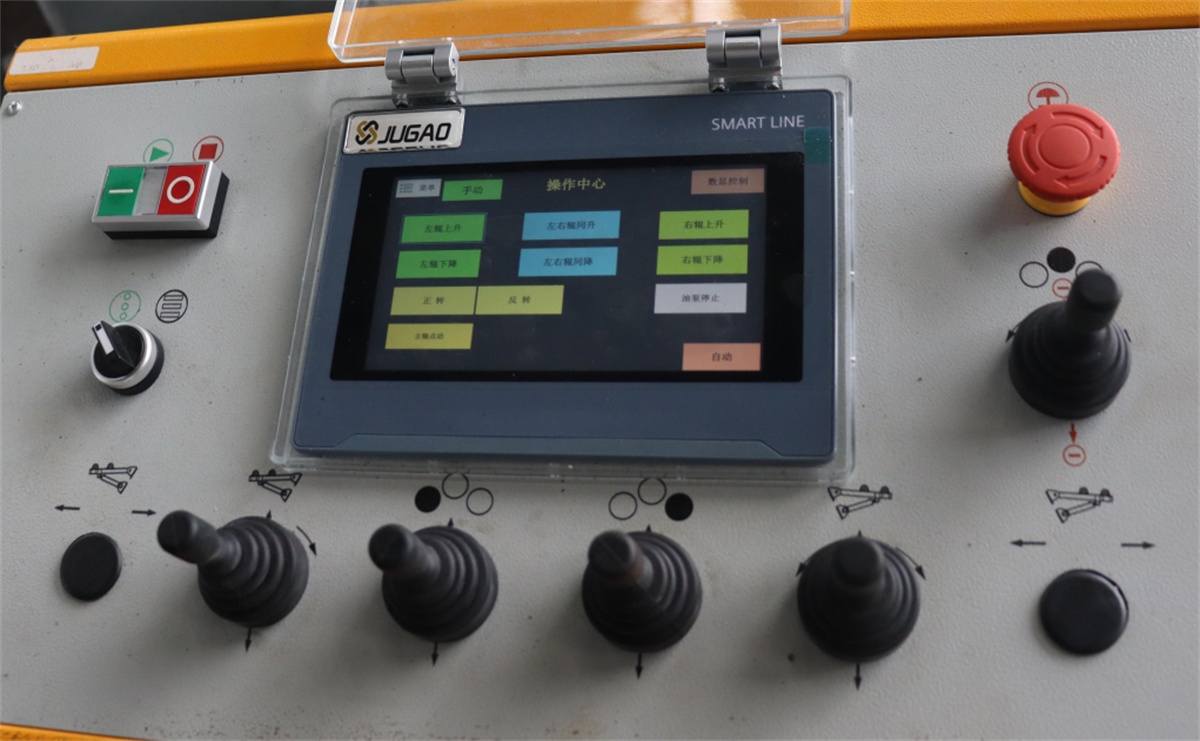
All actions should be centrally controlled through the control panel on the operating console. Unauthorized alteration of control circuits or parameter settings is strictly prohibited.
During bending, closely observe the deformation of the profile and the operating status of the equipment. Stop the machine immediately if any abnormality is detected.
Speed Control:
Control the speed during bending to avoid excessive speed leading to material tearing, excessive springback, or equipment overload.
Especially when bending profiles with large angles or small radii, appropriately reduce the speed to ensure forming quality and safety.
Loading and Unloading and Workpiece Handling:
Designated Personnel: Loading and unloading the workpieces must be directed and coordinated by a designated person to ensure the safety of operators and prevent squeezing or collisions.
Operate the air jack (cylinder or lifting device) switch only after hearing a clear start command. Arbitrary start and stop are strictly prohibited.
Workpiece Placement: Workpieces should be neatly placed, leveled, and securely positioned according to fixed-position management requirements to prevent rolling, slipping, or deformation. Do not adjust or support the profiles by hand while the equipment is running to avoid personal injury.
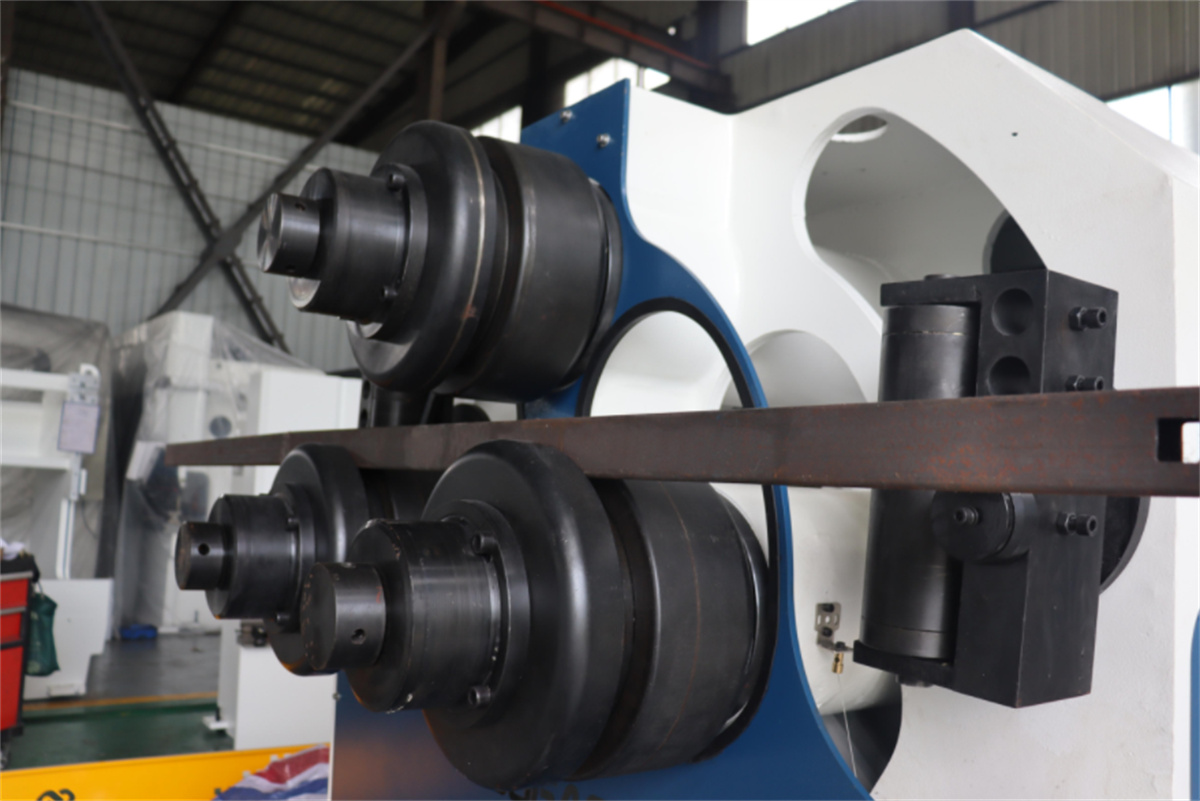
Large Bending Degree Processing: When the profile needs to be bent to a large degree or with a small radius of curvature, the operator and surrounding personnel must not stand near the end of the profile to prevent injury from material rebound or sudden slippage.
Shutdown and Maintenance
Normal Shutdown: After processing, first remove the profile, return the equipment to its initial or safe position, and then shut off the hydraulic system and power supply.
Perform daily cleaning as required, keeping the equipment and work area clean.
Regular Maintenance: Regularly inspect and maintain the hydraulic system, transmission components, and electrical system.
Regularly inspect the wear condition of easily worn parts such as rollers, support rollers, and wheels, and repair or replace them to ensure processing accuracy.
Summary
In conclusion, the profile bending machine is an important piece of equipment for bending metal profiles. With its reliable mechanical structure and advanced hydraulic control system, it can efficiently complete bending operations on various types of profiles. During use, the operating procedures must be strictly followed to ensure operational safety, processing quality, and equipment lifespan.

